Advantages of Working with an OEM RLC Load Bank Manufacturer
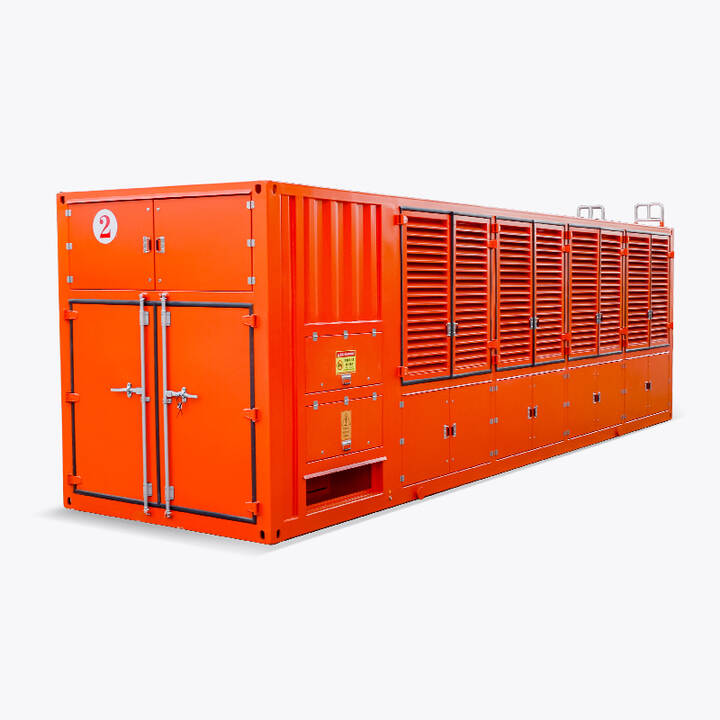
Choosing the right supplier is a critical step when investing in power testing equipment. RLC load banks are used to test generators, UPS systems, transformers, renewable energy systems, and other electrical infrastructure under realistic operating conditions. Because these applications demand accuracy and reliability, many organizations prefer to work directly with an Original Equipment Manufacturer (OEM). An OEM RLC load bank manufacturer designs, engineers, manufactures, and tests its own products, giving customers direct access to technical expertise and factory support.
Working with an OEM offers numerous advantages, from superior product quality to long-term service and customization. Below are the key benefits of partnering with an OEM RLC load bank manufacturer.
Direct Access to Product Expertise
One of the greatest advantages of working with an OEM RLC load bank manufacturer is direct access to the engineers who design and build the equipment.
OEM manufacturers have in-depth knowledge of:
- Product design
- Electrical performance
- System integration
- Operating principles
- Maintenance requirements
- Troubleshooting procedures
This expertise allows customers to receive accurate technical guidance throughout the purchasing, installation, and maintenance process.
High Product Quality
OEM manufacturers maintain full control over the manufacturing process. From raw material selection to final product testing, every stage follows strict quality control procedures.
By managing production internally, OEMs can ensure:
- Consistent manufacturing quality
- Reliable electrical performance
- Durable construction
- Long equipment lifespan
- Reduced manufacturing defects
This results in dependable load banks that perform reliably even in demanding industrial environments.
Custom-Designed Solutions
Every power system has unique testing requirements. Standard equipment may not always meet the needs of complex industrial applications.
An OEM manufacturer can develop customized RLC load banks based on factors such as:
- Power capacity
- Voltage requirements
- Frequency
- Power factor
- Cooling methods
- Control systems
- Installation environment
- Portable or stationary configurations
Customized equipment provides better performance because it is designed specifically for the intended application.
Advanced Engineering Capabilities
OEM manufacturers continuously invest in research and development to improve product performance.
A professional RLC load bank manufacturer incorporates modern technologies such as:
- Intelligent digital controls
- Remote monitoring
- Automated testing sequences
- Data logging
- Touchscreen interfaces
- Advanced protection systems
These innovations improve testing efficiency, simplify operation, and enhance overall equipment reliability.
Comprehensive Factory Testing
Before shipment, OEM manufacturers perform extensive factory testing to verify equipment performance.
Testing generally includes:
- Load verification
- Electrical performance checks
- Safety system testing
- Cooling system evaluation
- Control system validation
- Protection function testing
Factory testing ensures that every load bank operates according to design specifications before it reaches the customer.
Better Technical Support
When technical questions arise, working directly with the manufacturer provides faster and more accurate assistance.
OEM technical support teams understand every aspect of the equipment and can provide expert guidance on:
- Installation
- Commissioning
- Operation
- Troubleshooting
- Maintenance
- Software updates
This direct communication often leads to quicker problem resolution and reduced equipment downtime.
Genuine Spare Parts Availability
Maintenance and repairs require compatible replacement components.
An OEM RLC load bank manufacturer supplies genuine spare parts specifically designed for its equipment. Using original components helps maintain equipment performance, reliability, and safety while reducing the risk of compatibility issues.
Ready access to spare parts also minimizes repair delays and supports long-term equipment operation.
Strong Quality Assurance
OEM manufacturers implement comprehensive quality assurance programs throughout the production process.
Quality inspections are performed during:
- Material procurement
- Component assembly
- Electrical wiring
- Mechanical installation
- Performance testing
- Final inspection
These multiple checkpoints ensure every product meets high manufacturing standards before delivery.
Long-Term Partnership
Working with an OEM often leads to a long-term business relationship rather than a single equipment purchase.
As customer requirements evolve, the manufacturer can provide:
- Equipment upgrades
- Capacity expansions
- Additional load bank systems
- Technical training
- Preventive maintenance support
- Product improvements
This ongoing partnership helps organizations maintain reliable testing capabilities throughout the life of their electrical infrastructure.
Better Overall Value
Although the initial purchase price is important, long-term value is even more significant.
A trusted RLC load bank manufacturer delivers value through:
- Reliable equipment
- Lower maintenance costs
- Extended service life
- Accurate testing results
- Reduced downtime
- Responsive customer support
These benefits often result in lower total ownership costs over the equipment’s lifetime.
Confidence in Future Technology
OEM manufacturers continuously improve their products to meet changing industry demands. As power systems become more advanced, customers benefit from ongoing innovations in automation, digital controls, energy efficiency, and monitoring technologies.
This commitment to continuous improvement helps organizations stay prepared for future testing requirements.
Conclusion
Partnering with an OEM RLC load bank manufacturer offers significant advantages for organizations that require reliable and accurate power system testing. From superior engineering and customized solutions to comprehensive factory testing, genuine spare parts, and expert technical support, OEM manufacturers provide complete solutions that extend far beyond equipment supply. By working directly with an experienced OEM, businesses can improve testing accuracy, reduce maintenance costs, enhance equipment reliability, and build a long-term partnership that supports the evolving needs of their critical power infrastructure.